Heat exchanger fouling is the accumulation of unwanted deposits on heat transfer surfaces, caused mainly by scaling, crystallization, particulate deposition, biological growth, corrosion products, and chemical reaction. It reduces the overall heat transfer coefficient (U), increases pressure drop, raises energy consumption, and can eventually force unplanned shutdowns.
This guide explains exactly why fouling happens, how to predict it, and how to prevent or manage it in plate heat exchangers and shell and tube units. You will learn:
The six main fouling mechanisms and how each develops
How fouling affects U-value, pressure drop, and operating cost
Design and selection rules that reduce fouling risk
Chemical and mechanical cleaning methods compared
A step-by-step fouling prevention program
Common mistakes that accelerate fouling
Material, gasket, and maintenance decisions that extend service life
Quick Answer
| Question | Short Answer |
|---|---|
| What causes fouling? | Scaling, crystallization, particles, biological growth, corrosion, chemical reaction |
| Which exchanger fouls faster? | Plate heat exchangers foul faster with solids; shell and tube tolerate fouling better |
| How does fouling affect performance? | Lowers U, raises ΔP, increases energy cost, reduces capacity |
| How do you prevent fouling? | Correct velocity, filtration, water treatment, proper material, cleaning schedule |
| How do you clean a PHE? | CIP (clean-in-place) or manual plate opening |
| How do you clean an STHE? | Tube brushing, hydrojetting, or bundle removal |
| What is a typical fouling factor? | 0.0001–0.001 m²·K/W depending on fluid |
Table of Contents
What Is Heat Exchanger Fouling?
The 6 Main Fouling Mechanisms
How Fouling Affects Performance and Cost
Fouling Factors: How to Select Them
Design and Selection Rules to Reduce Fouling
How to Prevent Fouling: Step-by-Step Program
Cleaning Methods Compared
Material and Gasket Selection for Fouling Service
Comparison Tables
Fouling Prevention Checklist
Common Mistakes and How to Avoid Them
FAQ
Key Takeaways
What Is Heat Exchanger Fouling?
Heat exchanger fouling is the buildup of deposits on heat transfer surfaces that creates an additional thermal resistance and restricts flow. It is measured as a fouling factor (Rf) in m²·K/W and included in the overall heat transfer coefficient calculation.
Formula:
1/Udirty = 1/Uclean + Rf
Where:
Udirty = operating U after fouling
Uclean = U with clean surfaces
Rf = total fouling resistance (both sides)
Even a thin deposit layer can significantly reduce performance. For example, a 0.1 mm scale layer on a plate can cut U by 20–40%.
H3: Why Fouling Matters in Real Projects
Energy cost: Lower U means higher flow or higher temperature difference to compensate
Capacity loss: Fouled exchanger cannot meet design duty
Pressure drop: Deposits narrow flow channels, raising ΔP and pump power
Downtime: Cleaning stops production
Replacement cost: Severe fouling shortens equipment life
Safety: Overpressure, corrosion, and leaks can develop
The 6 Main Fouling Mechanisms
Fouling is not a single phenomenon. It develops through six distinct mechanisms, and each requires a different prevention strategy.
H3: 1. Crystallization (Scaling)
What it is: Dissolved salts precipitate onto hot surfaces when their solubility decreases with temperature.
Common examples:
Calcium carbonate (CaCO₃) in cooling water
Calcium sulfate (CaSO₄) in high-temperature service
Silica in boiler and geothermal water
Why it happens:
Temperature rise reduces solubility
pH change shifts carbonate equilibrium
Concentration exceeds saturation limit
Where it occurs most:
Hot side of exchangers
Cooling water circuits
Steam condensers
Boilers and evaporators
Prevention:
Water softening or demineralization
pH control (typically 7.5–8.5 for cooling water)
Scale inhibitors (phosphonates, polymers)
Limit surface temperature below scaling threshold
Periodic acid cleaning (compatible with material)
H3: 2. Particulate Fouling (Deposition)
What it is: Suspended solids settle or deposit on heat transfer surfaces.
Common examples:
Sand, silt, rust particles
River water or raw water solids
Process debris and fibers
Corrosion products from piping
Why it happens:
Low flow velocity allows settling
Filtration is inadequate
Upstream corrosion releases particles
Dead zones or low-flow areas exist
Where it occurs most:
Shell side of STHE (low velocity regions)
Inlet areas of PHE
Cooling water circuits
Open-loop systems
Prevention:
Install upstream filtration (50–200 micron depending on channel size)
Maintain velocity above settling threshold (typically > 0.5 m/s in tubes, > 0.3 m/s in plates)
Use wide-gap plates for dirty fluids
Avoid dead zones in piping and exchanger design
Flush systems before commissioning
H3: 3. Biological Fouling
What it is: Growth of microorganisms, algae, and biofilms on heat transfer surfaces.
Common examples:
Bacteria and biofilm in cooling water
Algae in open cooling systems
Fungi in humid or organic-rich environments
Why it happens:
Warm water and nutrients present
Stagnant or low-flow conditions
Inadequate biocide dosing
pH and oxygen levels favor growth
Where it occurs most:
Cooling towers and open circuits
Food and beverage exchangers
Marine and offshore systems
Data center cooling loops
Prevention:
Biocide treatment (oxidizing and non-oxidizing)
Maintain velocity to prevent stagnation
UV or ozone treatment where applicable
Regular cleaning and disinfection
Close-loop systems with proper water treatment
H3: 4. Corrosion Fouling
What it is: Corrosion products deposit on heat transfer surfaces, and the corrosion process itself roughens the surface.
Common examples:
Iron oxide (rust) from carbon steel piping
Copper corrosion products in mixed-metal systems
Galvanic corrosion from dissimilar metals
Why it happens:
Material incompatibility with fluid
Dissolved oxygen and chlorides present
Galvanic couple between dissimilar metals
Low pH or aggressive chemicals
Where it occurs most:
Systems with carbon steel and copper together
Seawater and chloride-rich environments
High-oxygen circuits
Poorly maintained closed loops
Prevention:
Select compatible materials (316L, titanium, SMO 254)
Use corrosion inhibitors
Maintain pH and oxygen control
Avoid dissimilar metal couples or use isolation
Regular water quality monitoring
H3: 5. Chemical Reaction Fouling
What it is: Deposits form from chemical reactions between process fluids or between fluid and surface material.
Common examples:
Polymerization of hydrocarbons at high temperature
Coke formation in refinery service
Decomposition of organic compounds
Why it happens:
High surface temperature triggers reaction
Reactive chemicals present
Long residence time at temperature
Where it occurs most:
Refinery and petrochemical exchangers
High-temperature oil circuits
Food processing (caramelization, protein denaturation)
Prevention:
Control surface temperature
Reduce residence time
Use fouling-resistant surface treatments
Add anti-coking or anti-polymerization additives
Design for easy cleaning
H3: 6. Solidification Fouling
What it is: Fluid freezes or solidifies on cold surfaces.
Common examples:
Wax deposition in crude oil
Ice formation in chillers
Freezing of process fluids at low temperature
Why it happens:
Surface temperature below freezing or pour point
Cold spots in the exchanger
Incorrect temperature control
Where it occurs most:
Chillers and refrigeration systems
Crude oil and waxy fluids
Cryogenic service
Cold-side surfaces
Prevention:
Maintain surface temperature above freezing point
Use antifreeze or pour-point depressants
Control coolant temperature carefully
Design for even flow distribution
Add temperature monitoring and alarms
How Fouling Affects Performance and Cost
Fouling degrades performance in three ways: lower U, higher ΔP, and reduced capacity.
H3: Effect on U-Value
| Fouling Level | U Reduction | Effect |
|---|---|---|
| Light (0.0001 m²·K/W) | 5–15% | Minor performance loss |
| Moderate (0.0003 m²·K/W) | 20–35% | Noticeable capacity loss |
| Heavy (0.0006 m²·K/W) | 40–55% | Significant underperformance |
| Severe (0.001 m²·K/W) | 60%+ | Exchanger cannot meet duty |
H3: Effect on Pressure Drop
Deposits narrow the flow channels. A 0.2 mm deposit in a 3 mm plate channel reduces flow area by roughly 13%, which can raise ΔP by 20–40% depending on the flow regime.
| Fouling Level | ΔP Increase |
|---|---|
| Light | 5–10% |
| Moderate | 15–30% |
| Heavy | 30–60% |
| Severe | 60%+ |
H3: Cost Impact
Fouling increases cost in four ways:
Energy cost: Pumps work harder, chillers and heaters run longer
Cleaning cost: Chemicals, labor, and downtime
Production loss: Reduced capacity or shutdown
Equipment replacement: Shortened service life
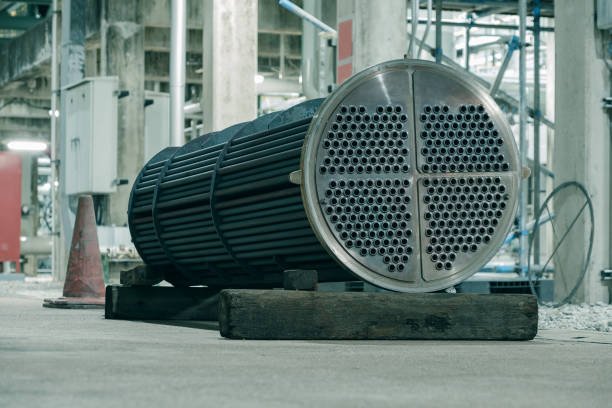
For a typical industrial exchanger, fouling-related costs can represent 10–25% of total operating cost. In severe cases, it is higher.
Fouling Factors: How to Select Them
Fouling factors (Rf) are added to the U calculation to account for expected deposit growth. They are not a safety margin — they represent real thermal resistance.
H3: Typical Fouling Factors
| Fluid | Rf (m²·K/W) | Notes |
|---|---|---|
| Clean water | 0.0001 | Treated, filtered |
| Cooling tower water | 0.0002–0.0004 | Depends on treatment |
| River water | 0.0004–0.0008 | Filtration required |
| Seawater | 0.0002–0.0005 | Material selection critical |
| Oil (light) | 0.0003–0.0005 | Temperature dependent |
| Oil (heavy) | 0.0005–0.001 | Preheating may help |
| Steam | 0.0001 | Clean steam |
| Process fluid with solids | 0.0005–0.001 | Filtration recommended |
| Refrigerant | 0.0001–0.0002 | Clean, closed loop |
| Brine / glycol | 0.0002–0.0004 | Concentration dependent |
H3: How to Use Fouling Factors
Add Rf to 1/Uclean for each side
Recalculate Udirty
Recalculate area: A = Q / (Udirty × LMTD × F)
Compare with clean area to see the fouling penalty
Example:
Uclean = 4,500 W/m²·K
Rf = 0.0002 each side (total 0.0004)
1/Udirty = 1/4,500 + 0.0004 = 0.000622
Udirty = 1,608 W/m²·K
Area increases from 5.3 m² to about 14.8 m² for the same duty. That is the real cost of fouling.
H3: Common Error
Do not add fouling factors that are too high. Excessive Rf leads to oversized exchangers, higher cost, and poor control at low load. Use realistic values based on actual water quality and operating experience.
Design and Selection Rules to Reduce Fouling
Design decisions made early have the biggest impact on fouling. Once the exchanger is built, options are limited.
H3: Velocity Rules
| Fluid Type | Minimum Velocity | Maximum Velocity |
|---|---|---|
| Water (tubes) | 1.0 m/s | 2.5 m/s |
| Water (plates) | 0.3 m/s | 1.5 m/s |
| Oil (tubes) | 0.5 m/s | 2.0 m/s |
| Process fluid with solids | 1.5 m/s | 3.0 m/s |
| Gas | 10 m/s | 30 m/s |
Why velocity matters: Higher velocity increases shear stress at the wall, which prevents particles from settling and reduces biofilm attachment. But too high a velocity causes erosion and high ΔP.
H3: Temperature Rules
Keep surface temperature below scaling threshold
Avoid hot spots by ensuring even flow distribution
For crystallization fouling, reduce temperature difference between fluid and surface
For solidification fouling, keep surface above pour point or freezing point
H3: Geometry Rules
| Fouling Type | Best Geometry |
|---|---|
| Scaling | Smooth surfaces, high velocity, PHE with wide channels |
| Particulate | Wide-gap plates, large tube diameter, STHE with removable bundle |
| Biological | Smooth surfaces, high velocity, easy CIP access |
| Corrosion | Corrosion-resistant material, no dead zones |
| Chemical reaction | Low residence time, easy cleaning |
| Solidification | Even flow, temperature control, avoid cold spots |
H3: Type Selection for Fouling Service
| Fouling Severity | Recommended Type |
|---|---|
| Light (clean water, treated) | Gasketed PHE |
| Moderate (cooling tower water) | Wide-gap PHE or STHE |
| Heavy (river water, solids) | STHE with removable bundle |
| Severe (slurries, fibers) | Wide-gap PHE or specialized STHE |
| Extreme (crystallizing, polymerizing) | STHE with online cleaning or spare unit |
How to Prevent Fouling: Step-by-Step Program
Fouling prevention is a program, not a single action. Follow these steps.
Step 1 — Identify the fouling mechanism.
Analyze fluid chemistry, temperature, and operating history. Determine whether the dominant mechanism is scaling, particulate, biological, corrosion, chemical reaction, or solidification.
Step 2 — Set water quality targets.
Define limits for hardness, pH, chlorides, suspended solids, and biological activity. Monitor regularly.
Step 3 — Install upstream treatment.
Filtration for particles
Softening or demineralization for hardness
Biocide dosing for biological growth
Corrosion inhibitors for metal protection
Scale inhibitors for crystallization
Step 4 — Design for adequate velocity.
Ensure flow velocity is above the settling threshold but below the erosion limit. Avoid dead zones and low-flow areas.
Step 5 — Select the right exchanger type.
Use wide-gap plates or STHE for dirty fluids. Use PHE only when fluid is clean and treatment is reliable.
Step 6 — Choose compatible materials.
Match wetted materials to fluid chemistry. Avoid galvanic couples.
Step 7 — Establish a cleaning schedule.
Base it on observed fouling rate. Monitor U and ΔP trends to predict when cleaning is needed.
Step 8 — Monitor performance continuously.
Track:
U-value decline
Pressure drop increase
Flow rate and temperature changes
Cleaning frequency
Step 9 — Clean before performance drops too far.
Early cleaning is easier and cheaper than late cleaning. Do not wait for a shutdown.
Step 10 — Review and improve.
After each cleaning, inspect deposits and adjust treatment, velocity, or schedule.
Cleaning Methods Compared
Cleaning method depends on exchanger type, fouling mechanism, and downtime tolerance.
H3: Chemical Cleaning (CIP)
| Aspect | Detail |
|---|---|
| Best for | Scaling, biological, light particulate |
| Method | Circulate cleaning solution through exchanger |
| Chemicals | Acid (scale), caustic (organic/bio), chelating agents |
| Downtime | Low (hours) |
| Frequency | High (routine) |
| Limitations | Not effective for heavy deposits or large solids |
| Material caution | Verify chemical compatibility with plates, gaskets, tubes |
H3: Mechanical Cleaning
| Aspect | Detail |
|---|---|
| Best for | Heavy particulate, hard scale |
| Method | Brushing, hydrojetting, scraping, drilling |
| Downtime | Moderate (hours to days) |
| Frequency | Lower (as needed) |
| Limitations | Can damage surfaces if done incorrectly |
| Material caution | Use soft brushes for titanium and stainless steel |
H3: Manual Plate Opening (PHE)
| Aspect | Detail |
|---|---|
| Best for | All fouling types in PHE |
| Method | Open frame, remove plates, clean individually |
| Downtime | Moderate (hours) |
| Frequency | As needed |
| Limitations | Gasket replacement may be required |
| Material caution | Inspect gaskets and plate surfaces |
H3: Bundle Removal (STHE)
| Aspect | Detail |
|---|---|
| Best for | Heavy fouling in shell side |
| Method | Remove tube bundle, clean outside and inside tubes |
| Downtime | High (days) |
| Frequency | Less frequent |
| Limitations | Requires space and lifting equipment |
| Material caution | Check tube sheet and baffle condition |
H3: Cleaning Method Selection Table
| Fouling Type | PHE | STHE |
|---|---|---|
| Scaling | CIP with acid | CIP or hydrojetting |
| Particulate | CIP or manual plate cleaning | Hydrojetting or bundle removal |
| Biological | CIP with biocide/caustic | CIP with biocide |
| Corrosion products | CIP with chelating agent | Hydrojetting |
| Chemical reaction | Manual plate cleaning | Bundle removal + mechanical |
| Solidification | Hot water or steam melt-out | Hot oil or steam melt-out |
Material and Gasket Selection for Fouling Service
Material choice affects both fouling resistance and cleaning compatibility.
H3: Material Selection
| Fluid / Condition | Recommended Material |
|---|---|
| Clean water, HVAC | 316L stainless steel |
| Cooling tower water | 316L, titanium |
| Seawater, chloride-rich | Titanium, SMO 254, duplex |
| Acids, aggressive chemicals | Nickel alloys, titanium, PTFE-lined |
| High-temperature steam | Carbon steel, chrome-moly |
| Food and beverage | 316L, FDA-compliant |
| Oil and hydrocarbon | Carbon steel, stainless steel |
H3: Gasket Selection (PHE)
| Gasket | Temp Range | Chemical Resistance | Best For |
|---|---|---|---|
| NBR | −20 to 110 °C | Good for water, oils | General HVAC, cooling |
| EPDM | −35 to 150 °C | Excellent for water, steam | Hot water, steam, glycol |
| HNBR | −20 to 160 °C | Good for oils, refrigerants | Refrigeration, oil cooling |
| FKM (Viton-compatible) | −20 to 200 °C | Excellent for chemicals | Aggressive fluids |
| PTFE-encapsulated | −20 to 180 °C | Exceptional | Highly corrosive fluids |
H3: Surface Treatment Options
Electropolishing: Smooths surface, reduces deposit adhesion
Coatings: PTFE, epoxy, or ceramic coatings for aggressive fluids
Surface hardening: For erosion resistance
Anodizing: For aluminum components (limited heat exchanger use)
Comparison Tables
Table 1: Fouling Mechanisms and Prevention Summary
| Mechanism | Cause | Best Prevention | Best Exchanger Type |
|---|---|---|---|
| Crystallization | Salt precipitation | Softening, pH control, inhibitors | Wide-gap PHE, STHE |
| Particulate | Suspended solids | Filtration, velocity control | STHE, wide-gap PHE |
| Biological | Microorganism growth | Biocide, UV, velocity | PHE with CIP, STHE |
| Corrosion | Material-fluid reaction | Material selection, inhibitors | Titanium, SMO 254, STHE |
| Chemical reaction | High-temp reaction | Temperature control, additives | STHE, easy-clean design |
| Solidification | Freezing/wax | Temperature control, additives | STHE, heated design |
Table 2: PHE vs STHE Fouling Comparison
| Parameter | Plate Heat Exchanger | Shell and Tube |
|---|---|---|
| Fouling tendency | Higher with solids | Lower |
| Channel size | 2–5 mm typical | 10–50 mm tubes |
| Cleaning | CIP or manual plate opening | Tube brushing, hydrojetting, bundle removal |
| Cleaning downtime | Short | Longer |
| Expansion | Add plates | Fixed |
| Best for clean fluids | Yes | Yes |
| Best for dirty fluids | No (unless wide-gap) | Yes |
| Fouling factor impact on area | High | Moderate |
| Inspection | Easy (open plates) | Requires bundle removal |
Fouling Prevention Checklist
Use this checklist to build a fouling prevention program.
- □
Identify dominant fouling mechanism from fluid analysis
- □
Set water quality targets (hardness, pH, chlorides, TSS)
- □
Install upstream filtration (50–200 micron)
- □
Implement water treatment (softening, biocide, inhibitors)
- □
Verify flow velocity above settling threshold
- □
Verify velocity below erosion limit
- □
Select exchanger type suitable for fouling severity
- □
Select materials compatible with fluid and cleaning chemicals
- □
Select gaskets compatible with temperature and chemicals
- □
Establish baseline U and ΔP at clean condition
- □
Monitor U and ΔP trends weekly or monthly
- □
Set cleaning trigger point (e.g., 15% U loss or 30% ΔP rise)
- □
Plan CIP or mechanical cleaning schedule
- □
Train operators on cleaning procedure and safety
- □
Keep spare gaskets and plates/tubes on site
- □
Review fouling history annually and adjust program
Common Mistakes and How to Avoid Them
1. Ignoring fouling during selection.
Fouling factors must be included in the U calculation from the start. Adding them later results in an undersized unit.
2. Using fouling factors that are too high.
Excessive Rf leads to oversized exchangers, higher cost, and poor control. Use realistic values.
3. Selecting a PHE for a dirty fluid.
Narrow plate channels block quickly. Use STHE or wide-gap PHE for solids-laden fluids.
4. Operating at low velocity.
Low velocity allows particles to settle and biofilm to grow. Maintain velocity above the settling threshold.
5. Skipping water treatment.
Untreated water causes scaling, corrosion, and biological growth. Treatment is cheaper than cleaning.
6. Cleaning too late.
Waiting until performance drops severely makes cleaning harder and more expensive. Clean at the trigger point.
7. Using the wrong cleaning chemical.
Incompatible chemicals can damage plates, gaskets, or tubes. Verify compatibility before cleaning.
8. Not monitoring performance.
Without U and ΔP trending, fouling is detected only when capacity fails. Monitor continuously.
9. Mixing dissimilar metals.
Galvanic corrosion accelerates fouling. Avoid dissimilar metal couples or use isolation.
10. Not keeping spare parts.
Without spare gaskets or plates, a fouling event becomes a long shutdown. Keep critical spares on site.
FAQ
1. What causes fouling in heat exchangers?
Fouling is caused by six main mechanisms: crystallization (scaling), particulate deposition, biological growth, corrosion products, chemical reaction, and solidification. Each mechanism requires a different prevention strategy.
2. How does fouling affect heat exchanger performance?
Fouling reduces the overall heat transfer coefficient (U), increases pressure drop, lowers capacity, and raises energy consumption. Severe fouling can force unplanned shutdowns.
3. What is a fouling factor?
A fouling factor (Rf) is a thermal resistance added to the U calculation to account for expected deposit growth. It is measured in m²·K/W and typically ranges from 0.0001 for clean water to 0.001 for heavy process fluids.
4. How do I prevent scaling in a heat exchanger?
Prevent scaling by softening or demineralizing water, controlling pH (typically 7.5–8.5), adding scale inhibitors, and keeping surface temperature below the scaling threshold.
5. Which heat exchanger is better for fouling service?
Shell and tube exchangers tolerate fouling better than plate heat exchangers because of larger flow channels and removable tube bundles. Wide-gap plate heat exchangers are an option for moderately dirty fluids.
6. How often should I clean my heat exchanger?
Cleaning frequency depends on fouling rate. Monitor U and ΔP trends and clean when U drops by 15% or ΔP rises by 30% from the clean baseline. Typical industrial exchangers need cleaning every 6–24 months.
7. What is the best way to clean a plate heat exchanger?
For light fouling, CIP (clean-in-place) with compatible chemicals is best. For heavy fouling, open the frame and clean plates manually. Always verify chemical compatibility with plate and gasket materials.
8. How do I clean a shell and tube heat exchanger?
Use tube brushing or hydrojetting for tube-side fouling. For shell-side fouling, remove the tube bundle and clean mechanically. Chemical cleaning can be used for light deposits.
9. Can fouling be completely prevented?
Fouling cannot be completely eliminated in most systems, but it can be significantly reduced through proper design, water treatment, velocity control, and cleaning schedules. The goal is to manage fouling, not eliminate it.
10. What is the most common fouling mistake?
The most common mistake is ignoring fouling during selection. Failing to include fouling factors in the U calculation leads to undersized exchangers and early performance problems.
11. How does velocity affect fouling?
Higher velocity increases wall shear stress, which prevents particle settling and reduces biofilm growth. However, excessive velocity causes erosion and high pressure drop. Maintain velocity within recommended ranges.
12. What materials resist fouling best?
Titanium, SMO 254, and duplex stainless steels resist corrosion fouling better than carbon steel or 316L in aggressive environments. Smooth surfaces such as electropolished stainless steel reduce deposit adhesion.
Key Takeaways
Heat exchanger fouling has six main causes: scaling, particulate deposition, biological growth, corrosion, chemical reaction, and solidification.
Fouling reduces U by 20–60%, increases pressure drop, and raises energy and maintenance costs.
Fouling factors must be included in the U calculation from the start — not added later.
Design decisions such as velocity, channel size, and material selection have the biggest impact on fouling resistance.
Shell and tube exchangers tolerate fouling better than plate heat exchangers; wide-gap plates are an option for moderately dirty fluids.
Water treatment, filtration, and biocide dosing prevent most fouling before it starts.
Monitor U and ΔP trends continuously and clean at the trigger point, not after performance fails.
Keep spare gaskets and plates or tubes on site to avoid long shutdowns.