Particles plug heat exchangers. It is that simple.
A unit that works fine on clean water or clear oil can fail in days when the stream carries sand, fibers, crystals, scale, or sludge. Channels block. Pressure drop rises. Flow drops. Production stops.
The fix is not a bigger pump or more frequent cleaning. It is selecting the right heat exchanger for the solids you actually have. That starts with the particle, not the equipment.
Why Particulate Streams Plug Heat Exchangers
Plugging happens when particles settle, bridge, agglomerate, or stick to surfaces. The smaller the flow passage, the faster it happens.
Common causes:
Settling: Dense particles fall out of suspension in low-velocity zones.
Bridging: Large or fibrous particles lock together at tube inlets, plate gaps, or nozzles.
Agglomeration: Sticky particles clump and form deposits.
Crystallization: Cooling causes solids to form on cold surfaces.
Fibrous material: Pulp, paper fiber, and biomass wrap around tubes and baffles.
Scale and corrosion products: Hard deposits narrow passages and trap other solids.
The result is always the same: higher pressure drop, lower flow, poor heat transfer, and unplanned downtime.
First: Characterize the Stream
Do not select a heat exchanger until you know what is in the fluid. A particle size distribution and a concentration number are not enough.
Collect this data:
| Data | Why it matters |
|---|---|
| Particle size distribution (D10, D50, D90) | Sets minimum flow passage |
| Maximum particle size | Prevents bridging at inlets and gaps |
| Particle shape | Fibers, flakes, and spheres behave differently |
| Particle density | Determines settling velocity |
| Solids concentration (% wt or % vol) | Affects viscosity, abrasion, and plugging |
| Fluid viscosity vs temperature | Controls flow and heat transfer |
| Temperature range | Affects crystallization, sticking, and material choice |
| pH and corrosivity | Materials and cleaning method |
| Abrasiveness | Erosion risk at high velocity |
| Flow rate and allowable pressure drop | Sizing and velocity limits |
| Cleaning method | CIP, reverse flow, manual, chemical |
| Duty cycle | Continuous, batch, startup, shutdown |
If the stream is fibrous, sticky, or crystallizing, say so early. Those are the hardest services.
Heat Exchanger Types for Particulate Service
There is no universal design. Each type has a range where it works.
| Type | Handles solids? | Best for | Avoid when |
|---|---|---|---|
| Shell and tube | Moderate | Large tubes, straight passages, removable bundle | Fibrous, sticky, or large solids |
| Wide-gap plate | Good | Slurries, fibers, easy cleaning | High pressure, very large particles |
| Spiral heat exchanger | Very good | Slurries, sludge, self-scouring | Very high pressure, abrasive solids |
| Scraped surface | Excellent | Viscous, sticky, crystallizing, high solids | Clean fluids, low cost priority |
| Fluidized bed | Excellent | Scaling, crystallization, fouling | Clean fluids, small duty |
| Plate and frame | Poor | Clean fluids only | Any significant solids |
| Double pipe / hairpin | Good | Small duties, large passages | Large duties, tight space |
| Air cooler | External fouling | Where water is unavailable | Dusty, fibrous air side |
Shell and Tube
Shell and tube can work for particulate streams if you design for it.
Use:
Large tube diameter (19 mm, 25 mm, or 38 mm)
Straight tubes, not U-bends
Removable bundle for cleaning
Vertical orientation with upflow
Few or no baffles on the shell side
Full-port nozzles and flush drains
Avoid small tubes, multi-pass designs, and shell-side flow where solids can settle.
Wide-Gap Plate Heat Exchanger
A wide-gap plate heat exchanger has larger channels than a standard plate unit. It handles fibrous and slurry streams better and opens easily for cleaning.
Typical gap: 6–12 mm. Some designs go wider.
Use it when:
Particles are small to medium
Cleaning access is important
Pressure and temperature are moderate
You need a compact footprint
Do not use it for large solids that can bridge the gap or for high-pressure service.
Spiral Heat Exchanger
A spiral heat exchanger has a single continuous channel on each side. There are no dead corners. Flow is highly turbulent, which helps keep particles moving.
It is a strong choice for:
Sludge and slurry
Wastewater
Fibrous material
Fouling streams
Small temperature approach
The single channel is easy to flush and clean. Pressure limits are lower than shell and tube, and very abrasive solids can erode the spiral.
Scraped Surface Heat Exchanger
A scraped surface heat exchanger uses rotating blades to keep the wall clean. It is the best choice when the product is viscous, sticky, crystallizing, or very high in solids.
It works for:
Crystallization
Sticky pastes
High-viscosity slurries
Heat-sensitive products
Cooling where solids form on the wall
It is more expensive and has rotating parts. But it keeps running when other designs plug.
Fluidized Bed Heat Exchanger
A fluidized bed heat exchanger circulates solid particles inside the tubes. The particles scrub the wall and prevent deposits.
It is used for:
Scaling water
Crystallizing solutions
Heavy fouling
Evaporators
It is specialized and not common in every plant, but it solves problems that other designs cannot.
Selection Rules That Prevent Plugging
1. Size the Passage for the Largest Particle
A common rule: minimum flow passage should be at least 3 times the maximum particle size. For fibrous or sticky material, go larger.
Examples:
1 mm particles: minimum 3 mm gap
5 mm particles: minimum 15 mm gap
Fibrous pulp: wide-gap or spiral, not standard plate
If the passage is too small, bridging is only a matter of time.
2. Keep Velocity Above Settling
Particles settle when velocity is too low. You need enough velocity to keep them suspended.
Typical slurry velocities:
Fine particles: 1.5–2.5 m/s
Dense or coarse particles: 2.5–3.5 m/s
Fibrous material: 2–4 m/s depending on consistency
But high velocity causes erosion. Balance transport against wear.
3. Use Vertical Upflow Where Possible
For settling slurries, vertical upflow is the safest orientation. Gravity works against deposition. Horizontal tubes and low points collect solids.
If horizontal flow is unavoidable, use periodic flushing and avoid long straight runs without drains.
4. Eliminate Dead Zones
Dead zones are where particles settle and bake.
No sharp corners
No low-flow pockets
No unused branches
Full-port nozzles
Smooth transitions
Drainable low points
5. Design for Cleaning
Assume you will need to clean. Make it easy.
Removable bundles
Hinged covers
Quick-release connections
CIP connections
Reverse flow capability
Access for hydroblasting or rodding
6. Choose Erosion-Resistant Materials
Particles wear metal. Harder materials last longer.
Stainless steel for mild service
Duplex and super duplex for corrosive slurries
Titanium for seawater and chlorides
Hard coatings for abrasive solids
Rubber or polymer linings for impact wear
Check velocity limits for each material. What works at 1.5 m/s may fail at 3 m/s.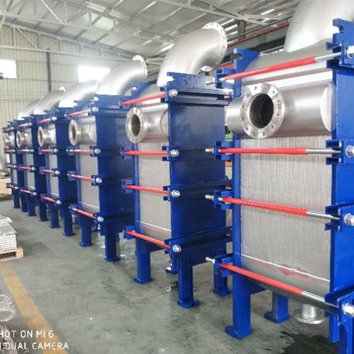
7. Add Redundancy
If cleaning is frequent, install two smaller units in parallel. One runs while the other is cleaned. This avoids production stops.
8. Monitor Pressure Drop
Pressure drop is your best plugging indicator. Trend it. When it rises above the cleaning threshold, act before flow stops.
Common Pain Points and Fixes
Plugging at the inlet
Enlarge nozzles. Add a flanged strainer only if it can be cleaned easily. Avoid small inlet openings.
Settling in horizontal tubes
Switch to vertical upflow. Increase velocity. Add periodic flush.
Fibrous material wrapping tubes
Use wide-gap plate, spiral, or scraped surface. Avoid shell and tube with baffles.
Crystallization on cold surfaces
Use scraped surface or fluidized bed. Control coolant temperature. Avoid high temperature difference.
Erosion at high velocity
Reduce velocity. Use harder materials. Replace elbows with long-radius bends.
Frequent cleaning downtime
Add parallel units. Improve cleaning access. Use online reverse flow.
High pressure drop after cleaning
Check for remaining deposits, damaged parts, or gasket protrusion. Verify flow rate.
FAQ
Can a plate heat exchanger handle particles?
Only a wide-gap plate design, and only if the largest particle is much smaller than the gap. Standard plate heat exchangers plug quickly.
What is the best heat exchanger for slurry service?
It depends on particle size, concentration, viscosity, and temperature. Spiral, wide-gap plate, scraped surface, and fluidized bed are the main options. Shell and tube can work with large tubes and straight passages.
How do I prevent heat exchanger plugging?
Size passages for the largest particle, keep velocity above settling, avoid dead zones, use vertical upflow, and design for cleaning.
What particle size can a shell and tube heat exchanger handle?
As a rule, maximum particle size should be no more than one-third of the tube diameter. For reliable operation, keep it smaller.
How often should I clean a particulate heat exchanger?
When pressure drop rises above a set threshold or flow drops. Monitor continuously. Do not wait for a fixed schedule.
Can I clean a plugged heat exchanger online?
Sometimes. Reverse flow, backflush, and CIP can help. Heavy plugging usually needs offline mechanical cleaning.
Bottom Line
Particulate streams punish the wrong heat exchanger. The right design keeps particles moving, avoids dead zones, and makes cleaning practical.
Start with the particle size, shape, concentration, and settling behavior. Choose a type that fits: wide-gap plate, spiral, scraped surface, fluidized bed, or a properly designed shell and tube. Then set velocity, orientation, materials, and cleaning access.
If you are selecting a heat exchanger for a particle-laden stream, send your particle size distribution, solids concentration, flow rate, temperatures, and current plugging problem. We will help you choose a design that stays open and keeps your process running.