Steam is expensive. If your plant runs an old heat exchanger, you are likely paying for steam you do not need.
Old units foul. Tubes erode. Controls drift. Steam traps fail. The heat exchanger that was once efficient now needs more steam to do the same job. The good news: you do not always need a new heat exchanger. A well-planned retrofit can cut steam use by 10–30% with a payback measured in months, not years.
This guide covers how to assess an old heat exchanger, where steam is wasted, and the retrofit options that actually pay.
Why Old Heat Exchangers Waste Steam
Steam waste rarely comes from one big failure. It comes from several small ones stacked together.
Common causes:
Fouling and scaling. Deposits add thermal resistance. The control valve opens wider to compensate. More steam, same duty.
Undersized area. The unit was sized for a lower duty or without proper fouling allowance. It cannot reach the target temperature without extra steam.
Wrong heat exchanger type. A shell and tube may be inefficient where a plate heat exchanger would achieve a closer temperature approach.
Poor temperature approach. A large approach means the process outlet is far from the steam temperature. Heat is left on the table.
Steam trap failures. Failed-open traps pass live steam. Failed-closed traps flood the exchanger. Both waste energy.
Air in the steam system. Air reduces heat transfer and lowers steam temperature. It must be vented.
Condensate not recovered. Hot condensate is dumped instead of returned to the boiler. Makeup water and chemicals cost money.
Control valve hunting. Oversized valves and poor tuning cause temperature swings and steam surges.
No heat integration. Hot process streams are cooled with water while steam heats other streams. Waste heat is ignored.
Insulation damage. Bare flanges, valves, and pipes lose heat. Steam consumption rises.
The first step is to find where the steam is going.
Step 1: Measure Before You Modify
Do not guess. Instrument the system and collect data.
Measure:
Steam flow rate to the heat exchanger
Steam pressure and temperature
Process inlet and outlet temperatures
Process flow rate
Condensate temperature and flow
Pressure drop across the heat exchanger
Ambient temperature
Calculate the current heat duty and compare it to the design duty. If the unit uses 20% more steam for the same duty, fouling or a mechanical problem is likely.
Check the temperature approach:
Approach = Steam saturation temperature − Process outlet temperature
A small approach means good performance. A large approach means the unit is not transferring heat efficiently.
For example, if steam is at 170°C and the process outlet is 120°C, the approach is 50°C. That is poor. A plate heat exchanger or a larger unit could reduce it to 10–15°C, cutting steam use.
Step 2: Quick Wins (Low Cost, Fast Payback)
Before spending capital, fix the basics.
1. Clean the heat exchanger.
Fouling is the number one cause of excess steam use. Chemical or mechanical cleaning can restore performance. Measure steam flow before and after. A 10–20% reduction is common.
2. Fix steam traps.
Test every trap. Replace failed-open traps immediately. Failed-closed traps cause flooding and poor heat transfer. A steam trap survey is one of the highest-return maintenance tasks in any plant.
3. Vent air and non-condensable gases.
Air in steam reduces the heat transfer coefficient and lowers steam temperature. Install automatic air vents at high points. Check that they work.
4. Insulate bare surfaces.
Flanges, valves, and exposed piping lose heat. Insulation blankets and lagging reduce losses. The payback is often under a year.
5. Recover condensate.
Return hot condensate to the boiler. Every 6°C (10°F) of condensate temperature recovered saves roughly 1% of boiler fuel. Condensate also reduces water treatment costs.
6. Tune the control loop.
Check the steam control valve. Is it oversized? Is it hunting? Tune the PID. A stable control loop uses less steam than one that swings.
7. Remove unnecessary bypasses.
Bypass valves that leak steam or allow flow around the exchanger waste energy. Fix or remove them.
8. Check for steam leaks.
A single 3 mm hole in a steam line can cost thousands per year. Walk the line and fix leaks.
Step 3: Retrofit and Upgrade Options
If quick wins are not enough, consider a retrofit. The right option depends on the duty, fluid, and space.
Add Surface Area
If the unit is undersized, adding tubes or plates increases area. More area means less steam for the same duty.
Shell and tube: Add tubes if the shell allows. Or add a second unit in series.
Plate heat exchanger: Add plates. Easy if the frame has spare capacity.
Replace with a Plate Heat Exchanger
Plate heat exchangers achieve much closer temperature approaches than shell and tube. A plate unit can reduce steam use by 15–30% in the same duty.
They are compact, easy to clean, and have high heat transfer coefficients. The trade-off is pressure drop and gasket compatibility. For clean fluids, it is often the best retrofit.
Install a Feed-Effluent Exchanger
Use the hot process outlet to preheat the cold process inlet. This reduces the steam needed to reach the target temperature.
For example, if the process outlet is at 120°C and the inlet is at 30°C, a feed-effluent exchanger can preheat the inlet to 80°C. The steam heater only needs to raise it from 80°C to 120°C. Steam use drops by 40%.
Add an Economizer
Use hot flue gas or another waste heat stream to preheat boiler feedwater or process fluid. This reduces steam demand in the boiler or the process.
Upgrade to High-Efficiency Tubes
Enhanced tubes with internal fins or twisted tape inserts increase turbulence and heat transfer. They can boost U-value by 20–50% in some services. They also reduce fouling by increasing wall shear.
Use Turbulence Promoters
For shell and tube units with laminar flow, inserts like twisted tape or static mixers increase turbulence. This improves heat transfer and reduces steam use. Check pressure drop and cleaning.
Install a Steam Ejector or Thermocompressor
If you have high-pressure steam and low-pressure steam, a thermocompressor can reuse low-pressure steam. This reduces the amount of high-pressure steam needed.
Consider Mechanical Vapor Recompression (MVR)
For evaporation or distillation, MVR compresses overhead vapor to reuse its latent heat. It can cut steam use dramatically, but it is a larger project with higher capital cost.
Step 4: Control and Operation
Even a good heat exchanger wastes steam if it is operated poorly.
Optimize the temperature setpoint.
Do you really need 120°C? If 110°C works, lower the setpoint. Every degree counts.
Reduce steam pressure.
Lower steam pressure reduces the saturation temperature. If the process allows, use lower-pressure steam. This can also reduce flash losses.
Use a cascade control.
Control the process outlet temperature by adjusting steam flow. Avoid controlling steam pressure directly, which can cause overheating.
Install a steam flow meter.
You cannot manage what you do not measure. A flow meter shows the impact of every change.
Check for oversizing.
An oversized heat exchanger with a small duty can run at low velocity, which causes fouling. It also wastes steam if the control valve cannot turn down properly.
Schedule cleaning based on data.
Use pressure drop and temperature approach to plan cleaning. Do not wait for production loss.
Step 5: Heat Integration and Waste Heat Recovery
Look beyond the single heat exchanger. The plant has many heat sources and sinks.
Pinch analysis.
A pinch study identifies the minimum steam and cooling water use for the whole plant. It shows where heat can be recovered between streams.
Use waste heat for preheating.
Hot wastewater, flue gas, and product streams can preheat boiler feedwater or process fluids.
Recover flash steam.
High-pressure condensate flashes to low-pressure steam when discharged. Use it in a low-pressure steam header instead of venting.
Use a heat pump.
For low-temperature waste heat, a heat pump can upgrade it to a useful temperature. This is often more efficient than burning more steam.
Payback Calculation
Any retrofit must pay for itself. Calculate the savings and the cost.
Annual steam savings:
Steam saved (kg/hr) × operating hours × steam cost ($/kg)
Example: 500 kg/hr saved, 8,000 hours/year, $30/tonne steam.
Savings = 500 × 8,000 × 0.03 = $120,000 per year
If the retrofit costs $150,000, the payback is 1.25 years. That is a strong project.
Include:
Capital cost (equipment, installation, controls)
Energy savings (steam, cooling water, electricity)
Maintenance savings (less fouling, fewer repairs)
Production gains (more capacity, better quality)
Prioritize projects with payback under two years. Start with quick wins, then move to capital projects.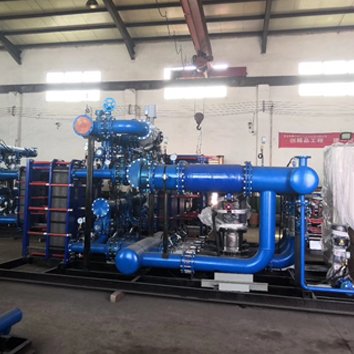
Common Mistakes
Retrofitting without measuring.
You cannot prove savings if you do not have a baseline.
Oversizing the new unit.
Too much area lowers velocity and causes fouling. Size for the duty plus a reasonable margin.
Ignoring pressure drop.
A new plate heat exchanger may save steam but increase pump energy. Check the total cost.
Forgetting the steam system.
A new heat exchanger will not help if steam traps are failed and pipes are uninsulated. Fix the system first.
Not involving operations.
The best design fails if operators do not understand how to run it. Train them.
Skipping the payback analysis.
Every project should have a clear financial case. If it does not pay back, do not do it.
FAQ
How much steam can a heat exchanger retrofit save?
Typically 10–30%. Cleaning alone can restore 10–20%. Replacing a shell and tube with a plate heat exchanger can save 15–30%. Feed-effluent exchangers can save 30–50% on the heater duty.
What is the fastest payback retrofit?
Steam trap repair, cleaning, insulation, and air venting. These often pay back in weeks or months.
Can I retrofit an old shell and tube heat exchanger?
Yes. Options include adding tubes, installing turbulence promoters, adding a second unit in series, or replacing the bundle with a high-efficiency design. Sometimes replacing it with a plate heat exchanger is better.
How do I know if my heat exchanger is wasting steam?
Compare actual steam flow to design. Check temperature approach. If the approach is more than 15–20°C, the unit is likely fouled or undersized.
What is the best way to reduce steam use in a distillation column?
Optimize reflux ratio, improve feed preheating, use a feed-effluent exchanger, and consider a reboiler retrofit with a closer temperature approach.
Do I need a new heat exchanger or just a cleaning?
Start with cleaning and steam system repairs. If performance does not return to baseline, then consider a retrofit or replacement.
Bottom Line
Old heat exchangers waste steam for predictable reasons: fouling, failed traps, poor control, and outdated design. The fix does not always require a new unit.
Measure the system. Fix the quick wins. Then consider a retrofit—plate heat exchanger, feed-effluent exchanger, enhanced tubes, or heat integration. Calculate the payback. Prioritize the projects that pay.
If you are planning a heat exchanger retrofit to cut steam use, send your current steam flow, process temperatures, flow rates, and heat exchanger details. We will help you identify the savings potential and recommend a retrofit that pays for itself.