Heat exchanger selection calculation is the process of determining the right exchanger type, size, and configuration by calculating heat duty, log mean temperature difference (LMTD), overall heat transfer coefficient (U), required area, and pressure drop. A correct calculation prevents oversizing, undersizing, premature fouling, and unnecessary cost.
This guide gives you the actual formulas, worked examples, parameter tables, and decision criteria used in real projects. You will learn:
The core selection calculation steps from duty to final model
How to calculate LMTD, U-value, and required heat transfer area
How to check pressure drop, fouling, and temperature approach
How to select materials, gaskets, and configurations
Common calculation mistakes and how to avoid them
Cost, lead time, and certification factors that affect selection
Quick Answer
| Calculation Step | Formula / Method |
|---|---|
| Heat duty | Q = ṁ × cp × ΔT |
| LMTD | ΔTlm = (ΔT1 − ΔT2) / ln(ΔT1 / ΔT2) |
| Required area | A = Q / (U × ΔTlm × F) |
| Pressure drop check | ΔP ≤ allowable ΔP per side |
| Fouling check | Include fouling factor Rf in U calculation |
| Final selection | Match area, ΔP, materials, and certifications |
Table of Contents
What Is Heat Exchanger Selection Calculation?
Step 1: Calculate Heat Duty (Q)
Step 2: Calculate LMTD and Correction Factor
Step 3: Determine Overall Heat Transfer Coefficient (U)
Step 4: Calculate Required Heat Transfer Area
Step 5: Check Pressure Drop
Step 6: Apply Fouling Factors
Step 7: Select Exchanger Type and Configuration
Step 8: Select Materials and Gaskets
Step-by-Step Selection Calculation Example
Comparison Tables
Pre-Selection Checklist
Common Mistakes and How to Avoid Them
Cost, Lead Time, and Certification Factors
FAQ
Key Takeaways
What Is Heat Exchanger Selection Calculation?
Heat exchanger selection calculation is a structured engineering method to size and choose an exchanger that meets a thermal duty within pressure, temperature, fouling, and cost constraints. It combines thermodynamics, fluid mechanics, and material selection into one decision.
The calculation answers five core questions:
How much heat must be transferred? (Q)
What is the driving temperature difference? (LMTD)
How effective is the heat transfer surface? (U)
How much area is needed? (A)
Will pressure drop and fouling allow it to work? (ΔP, Rf)
If any of these is wrong, the exchanger will underperform, foul early, or cost more than necessary.
Step 1: Calculate Heat Duty (Q)
Heat duty is the amount of heat transferred per unit time. It is the starting point of every selection calculation.
Formula:
Q = ṁ × cp × ΔT
Where:
Q = heat duty (W or kW)
ṁ = mass flow rate (kg/s)
cp = specific heat capacity (J/kg·K)
ΔT = temperature change of the fluid (K)
Alternative for phase change:
Q = ṁ × hfg
Where hfg is the latent heat of vaporization or condensation (J/kg).
H3: Example — Water Heating
ṁ = 5 kg/s
cp = 4,180 J/kg·K
ΔT = 20 K (from 30 °C to 50 °C)
Q = 5 × 4,180 × 20 = 418,000 W = 418 kW
H3: Why This Step Matters
An error in Q propagates through every later calculation. Always confirm:
Mass flow is in kg/s, not L/min
cp is at the correct mean temperature
ΔT is the actual process requirement, not assumed
Step 2: Calculate LMTD and Correction Factor
LMTD (log mean temperature difference) is the effective temperature driving force between the two fluids.
Formula for counter-current flow:
ΔTlm = (ΔT1 − ΔT2) / ln(ΔT1 / ΔT2)
Where:
ΔT1 = hot inlet − cold outlet
ΔT2 = hot outlet − cold inlet
H3: Example — Counter-Current
Hot side: 90 °C → 60 °C
Cold side: 20 °C → 50 °C
ΔT1 = 90 − 50 = 40 K
ΔT2 = 60 − 20 = 40 K
ΔTlm = (40 − 40) / ln(40/40) → use arithmetic mean = 40 K
For unequal values:
ΔT1 = 50, ΔT2 = 20
ΔTlm = (50 − 20) / ln(50/20) = 30 / 0.916 = 32.7 K
H3: Correction Factor F for Multi-Pass Designs
For shell and tube with multiple tube passes or cross-flow, multiply by a correction factor F:
A = Q / (U × ΔTlm × F)
F is typically 0.8–1.0. If F < 0.75, the design is inefficient — consider more shells in series.
Step 3: Determine Overall Heat Transfer Coefficient (U)
U represents how well heat moves from one fluid to the other through the wall. It depends on fluid properties, flow velocity, and wall material.
Formula:
1/U = 1/hh + Rfh + t/k + Rfc + 1/hc
Where:
hh, hc = convective heat transfer coefficients (hot, cold)
Rfh, Rfc = fouling factors
t = wall thickness
k = wall thermal conductivity
H3: Typical U-Values
| Duty | U (W/m²·K) |
|---|---|
| Water–water (PHE) | 3,000–7,000 |
| Water–water (STHE) | 500–1,500 |
| Steam–water | 800–6,000 |
| Oil–water | 100–1,000 |
| Gas–liquid | 20–300 |
| Air–air | 10–50 |
H3: How to Improve U
Increase flow velocity (raises h, but also ΔP)
Use corrugated or enhanced surfaces
Reduce wall thickness where pressure allows
Keep fouling factors realistic — not oversized
Step 4: Calculate Required Heat Transfer Area
Area is the core output of selection calculation.
Formula:
A = Q / (U × ΔTlm × F)
H3: Example
Q = 418,000 W
U = 4,000 W/m²·K (PHE, water–water)
ΔTlm = 40 K
F = 1.0
A = 418,000 / (4,000 × 40 × 1.0) = 2.61 m²
For a shell and tube with U = 900 W/m²·K:
A = 418,000 / (900 × 40 × 1.0) = 11.6 m²
The plate exchanger needs ~4.5× less area for the same duty — this is the main reason PHEs are compact.
H3: Adding Safety Margin
Typical design margin:
Clean service: 10–15%
Moderate fouling: 15–25%
Heavy fouling: 25–40%
Margin that is too high raises cost and can cause control problems. Margin that is too low causes shortfall.
Step 5: Check Pressure Drop
Pressure drop determines pump power and operating cost. A design that meets thermal duty but exceeds allowable ΔP is not acceptable.
H3: Typical Allowable Pressure Drop
| Service | Allowable ΔP |
|---|---|
| Pumped liquid | 50–100 kPa |
| Cooling water | 30–80 kPa |
| Steam | 10–30 kPa |
| Gas | 1–5 kPa |
| Viscous fluid | 100–150 kPa |
H3: How to Estimate ΔP
Plate heat exchanger:
ΔP ≈ f × (L/de) × (ρ × v² / 2)
Where f depends on chevron angle and Reynolds number.
Shell and tube (tube side):
ΔP = (4 × f × L × n / d) × (ρ × v² / 2)
Where:
f = friction factor
L = tube length
n = number of passes
d = tube inner diameter
v = velocity
H3: Practical Rule
Increase passes → higher ΔP
Increase plate chevron angle → higher U but higher ΔP
Increase tube count → lower ΔP but lower velocity and U
Always verify ΔP with the vendor’s selection software before finalizing.
Step 6: Apply Fouling Factors
Fouling adds thermal resistance and reduces U over time. Ignoring it is a common cause of underperformance.
H3: Typical Fouling Factors
| Fluid | Rf (m²·K/W) |
|---|---|
| Clean water | 0.0001 |
| Cooling tower water | 0.0002–0.0004 |
| River water | 0.0004–0.0008 |
| Oil | 0.0003–0.0006 |
| Steam | 0.0001 |
| Process fluid with solids | 0.0005–0.001 |
H3: Effect on U
If Rf is added to 1/U, a small fouling factor can significantly reduce U. For example:
Clean U = 4,000 W/m²·K
Rf = 0.0002 m²·K/W (both sides)
1/Udirty = 1/4,000 + 0.0002 = 0.00025 + 0.0002 = 0.00045
Udirty = 2,222 W/m²·K
U drops by nearly half. This is why fouling must be included from the start.
Step 7: Select Exchanger Type and Configuration
Selection depends on the calculated duty, pressure, temperature, fouling, and space.
H3: Type Selection Logic
| Condition | Recommended Type |
|---|---|
| Clean fluids, close approach, low pressure | Gasketed PHE |
| High pressure, high temperature | Shell and tube |
| Aggressive fluids, no gaskets allowed | Brazed or welded PHE |
| Heavy fouling, solids present | Shell and tube or wide-gap PHE |
| Steam condensation | Shell and tube or welded PHE |
| Refrigerant evaporator/condenser | Brazed PHE |
| Large duty (> 5 MW) | Shell and tube |
| Limited space | PHE |
H3: Configuration Choices
Number of passes: more passes = higher velocity = higher U and ΔP
Flow arrangement: counter-current is most efficient
Shell type: fixed tube sheet, U-tube, floating head
Plate pattern: chevron angle (high or low theta)
Step 8: Select Materials and Gaskets
Material selection affects corrosion life, cost, and lead time.
H3: Plate and Tube Materials
| Fluid | Material |
|---|---|
| Clean water, HVAC | 316L stainless steel |
| Seawater, chloride | Titanium, SMO 254, duplex |
| Ammonia | Carbon steel (STHE), 316L (PHE) |
| Food and beverage | 316L, FDA-compliant |
| Acids, aggressive chemicals | Nickel alloys, titanium |
| High-temperature steam | Carbon steel, chrome-moly |
H3: Gasket Selection (PHE)
| Gasket | Temp Range | Best For |
|---|---|---|
| NBR | −20 to 110 °C | Water, oils, HVAC |
| EPDM | −35 to 150 °C | Hot water, steam, glycol |
| HNBR | −20 to 160 °C | Oils, refrigerants |
| FKM (Viton-compatible) | −20 to 200 °C | Aggressive chemicals |
| PTFE-encapsulated | −20 to 180 °C | Highly corrosive fluids |
Step-by-Step Selection Calculation Example
Problem: Cool 10 kg/s of water from 80 °C to 50 °C using cooling water entering at 25 °C and leaving at 45 °C. Allowable ΔP: 80 kPa both sides. Fluid is clean.
Step 1 — Heat duty:
Q = 10 × 4,180 × (80 − 50) = 1,254,000 W = 1,254 kW
Step 2 — LMTD:
ΔT1 = 80 − 45 = 35 K
ΔT2 = 50 − 25 = 25 K
ΔTlm = (35 − 25) / ln(35/25) = 10 / 0.336 = 29.8 K
Step 3 — U-value:
Assume PHE water–water U = 4,500 W/m²·K (clean, with margin)
Step 4 — Required area:
A = 1,254,000 / (4,500 × 29.8 × 1.0) = 9.35 m²
Add 15% margin → 10.75 m²
Step 5 — Pressure drop check:
Select a PHE model with 10.75 m² and verify ΔP ≤ 80 kPa. Adjust plate count or chevron angle if needed.
Step 6 — Fouling:
Apply Rf = 0.0001 each side. Recalculate U. If U drops to ~3,800 W/m²·K, area becomes:
A = 1,254,000 / (3,800 × 29.8) = 11.1 m²
Step 7 — Material:
316L plates, EPDM gaskets (water, 80 °C max).
Step 8 — Final selection:
A gasketed PHE with ~11–12 m² effective area, 316L/EPDM, ΔP within 80 kPa.
 Comparison Tables
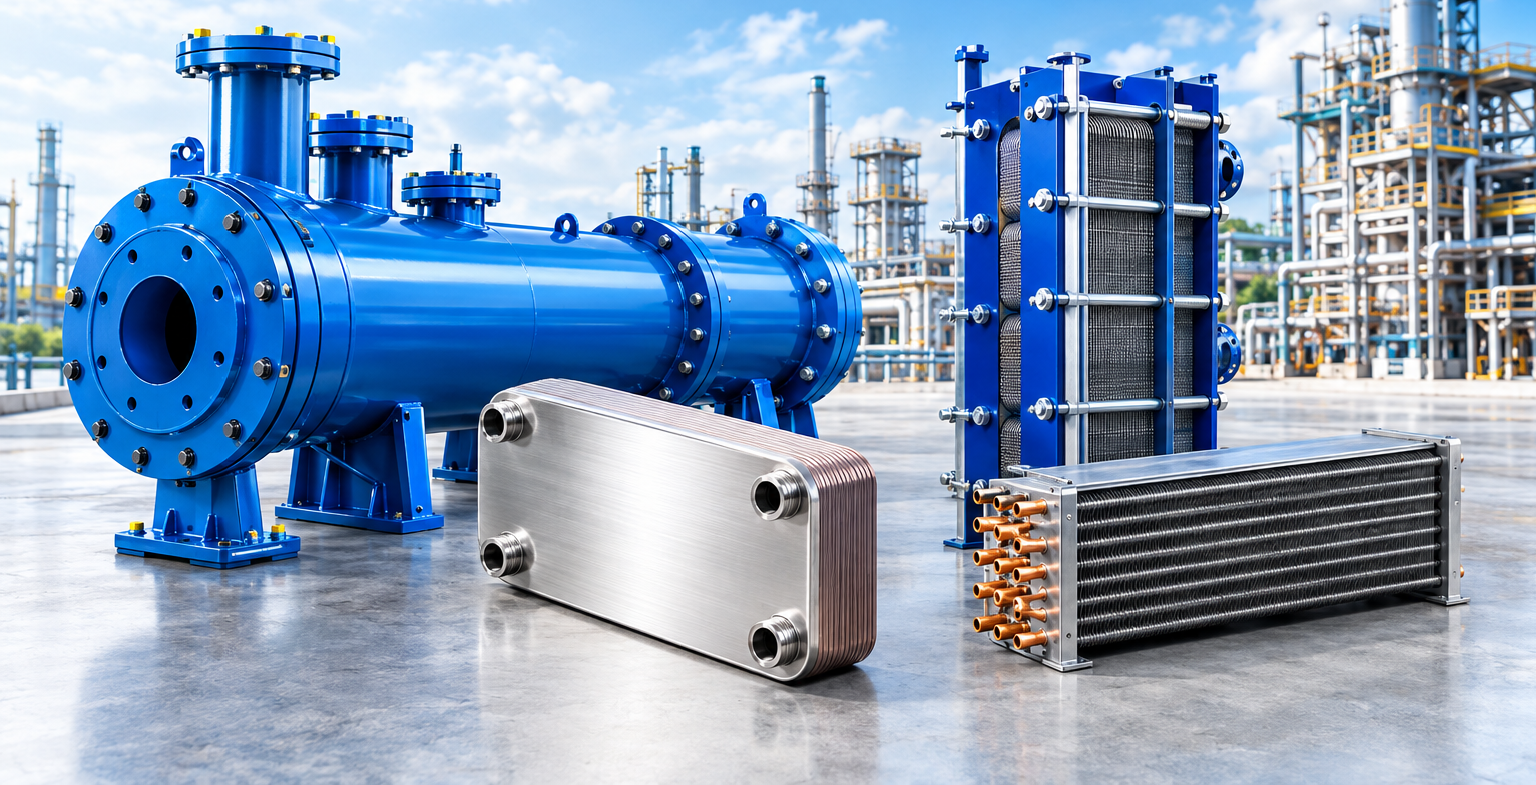 Comparison Tables
Table 1: PHE vs STHE for Selection Calculation
| Parameter | Plate Heat Exchanger | Shell and Tube |
|---|---|---|
| Typical U (water–water) | 3,000–7,000 W/m²·K | 500–1,500 W/m²·K |
| Temperature approach | 1–3 °C | 5–10 °C |
| Max pressure | ~25 bar (gasketed) | 100+ bar |
| Max temperature | ~200 °C | 600 °C+ |
| Fouling tolerance | Lower | Higher |
| Area for 1,254 kW example | ~11 m² | ~35–45 m² |
| Cleaning | CIP or plate opening | Tube cleaning |
| Expansion | Add plates | Fixed |
Table 2: Design Margin Selection
| Service Condition | Recommended Margin |
|---|---|
| Clean, well-defined fluids | 10–15% |
| Moderate fouling, some uncertainty | 15–25% |
| Heavy fouling, phase change, high viscosity | 25–40% |
| Future capacity expansion planned | 20–30% + expandable frame |
Pre-Selection Checklist
- □
Heat duty (Q) calculated and verified
- □
Fluid properties confirmed at mean temperature
- □
Inlet and outlet temperatures confirmed for both sides
- □
LMTD and correction factor F calculated
- □
U-value estimated from reliable data
- □
Required area calculated with margin
- □
Allowable pressure drop specified per side
- □
Fouling factors selected
- □
Exchanger type chosen (PHE, STHE, brazed, welded)
- □
Material and gasket selected
- □
Certification requirements identified (PED, ASME, etc.)
- □
Footprint and maintenance access verified
- □
Vendor thermal calculation and drawing requested
- □
Spare parts and service support confirmed
Common Mistakes and How to Avoid Them
1. Using L/min instead of kg/s for mass flow.
Unit errors are the most common cause of wrong duty. Always convert to SI units first.
2. Ignoring the LMTD correction factor.
For multi-pass or cross-flow designs, F < 1.0 must be applied. Ignoring it oversizes or undersizes the unit.
3. Using clean U without fouling.
Fouling can cut U by 30–50%. Always include Rf.
4. Selecting U from memory instead of data.
U varies with velocity, viscosity, and geometry. Use vendor data or validated correlations.
5. Underspecifying pressure drop.
A design that meets duty but exceeds ΔP will fail. Specify ΔP limits before selection.
6. Applying too much safety margin.
Oversizing raises cost and can cause control instability, especially in close-approach duties.
7. Choosing PHE for fouling fluids.
Narrow plate channels block easily. Use STHE or wide-gap PHE for solids-laden fluids.
8. Forgetting thermal expansion.
High ΔT causes differential expansion. Use U-tube or floating head STHE, or PHE with proper frame design.
9. Mismatching materials.
Dissimilar metals cause galvanic corrosion. Verify material compatibility with the fluid.
10. Skipping certification planning.
PED, ASME, or marine approvals affect design, material, and lead time. Plan early.
Cost, Lead Time, and Certification Factors
H3: Cost Drivers
| Factor | Impact |
|---|---|
| Heat transfer area | Direct cost driver |
| Material (316L vs titanium) | 1.5–4× cost difference |
| Pressure rating | Higher pressure = thicker plates/tubes |
| Gasket material | FKM/PTFE higher than EPDM |
| Certification | Adds engineering and inspection cost |
| Custom vs standard | Custom adds 20–50% |
H3: Lead Time Factors
| Item | Typical Lead Time |
|---|---|
| Standard PHE | 2–4 weeks |
| Custom PHE | 4–8 weeks |
| Standard STHE | 6–10 weeks |
| Custom STHE (exotic material) | 10–16 weeks |
| Certification (PED, ASME) | +2–6 weeks |
H3: Certification Requirements by Market
| Market | Requirement |
|---|---|
| Europe | PED 2014/68/EU, CE marking, EN 13445 |
| North America | ASME Section VIII, U-stamp, CRN |
| Middle East | ASME, PED, local authority |
| Southeast Asia | ASME, PED, national standards |
| Marine | ABS, DNV, Lloyd’s Register |
| Food / pharma | FDA, 3-A, EHEDG |
FAQ
1. What is the formula for heat exchanger selection calculation?
The core formula is A = Q / (U × LMTD × F), where Q is heat duty, U is overall heat transfer coefficient, LMTD is log mean temperature difference, and F is the correction factor. Q itself is calculated as ṁ × cp × ΔT.
2. How do I calculate heat exchanger area?
Divide the heat duty by the product of U-value and LMTD: A = Q / (U × ΔTlm). Add a design margin of 10–25% depending on fouling risk.
3. What is a good temperature approach for a heat exchanger?
Plate heat exchangers can achieve 1–3 °C approach. Shell and tube typically need 5–10 °C for economical design. Closer approach means larger area and higher cost.
4. How do I choose between plate and shell and tube?
Choose plate for clean fluids, close approach, low pressure, and compact space. Choose shell and tube for high pressure, high temperature, heavy fouling, and large duties.
5. What U-value should I use for water-to-water?
For plate heat exchangers, 3,000–7,000 W/m²·K. For shell and tube, 500–1,500 W/m²·K. Always confirm with vendor data for your specific velocity and geometry.
6. How much safety margin should I add?
10–15% for clean service, 15–25% for moderate fouling, and 25–40% for heavy fouling or phase change. Avoid excessive margin — it raises cost and can cause control issues.
7. What is the LMTD correction factor F?
F accounts for non-ideal flow arrangements in multi-pass or cross-flow exchangers. It is typically 0.8–1.0. If F < 0.75, redesign with more shells in series.
8. How do I calculate pressure drop?
Pressure drop depends on flow velocity, channel geometry, and fluid properties. Use vendor selection software or standard correlations (Darcy-Weisbach for tubes, plate-specific correlations for PHEs).
9. What fouling factor should I use?
Clean water: 0.0001 m²·K/W. Cooling tower water: 0.0002–0.0004. River water: 0.0004–0.0008. Oil: 0.0003–0.0006. Always match to actual water quality or process fluid.
10. Can I add capacity later?
Plate heat exchangers can often be expanded by adding plates if the frame has spare capacity. Shell and tube units generally cannot be expanded and may need replacement.
11. How does material selection affect cost?
316L stainless steel is standard. Titanium, SMO 254, and nickel alloys cost 1.5–4× more but are required for seawater, chlorides, and aggressive chemicals.
12. What certifications affect heat exchanger selection?
PED (Europe), ASME Section VIII (North America), CRN (Canada), and marine class approvals (ABS, DNV) affect design, material, testing, and lead time. Plan certification early.
Key Takeaways
Heat exchanger selection calculation starts with heat duty Q = ṁ × cp × ΔT and ends with a verified model that meets thermal, pressure, and fouling requirements.
The core sizing formula is A = Q / (U × LMTD × F). Errors in any input propagate through the entire design.
Fouling factors must be included from the start — they can reduce U by 30–50%.
Pressure drop must be checked separately from thermal duty; a design that meets Q but exceeds ΔP is not acceptable.
Design margin should match fouling risk: 10–15% for clean service, up to 40% for heavy fouling.
Material and gasket selection depend on fluid, temperature, and certification requirements.
Certification (PED, ASME, marine) affects design, cost, and lead time — plan it early.
Always request a vendor thermal calculation and drawing before finalizing your selection.