Description


| No. | Feature | Description |
|---|---|---|
| 01 | High-Quality Material Selection | Fine material selection and production; product quality assurance; long service life. |
| 02 | Fine Processing | Mature technology; high-standard production; precision manufacturing. |
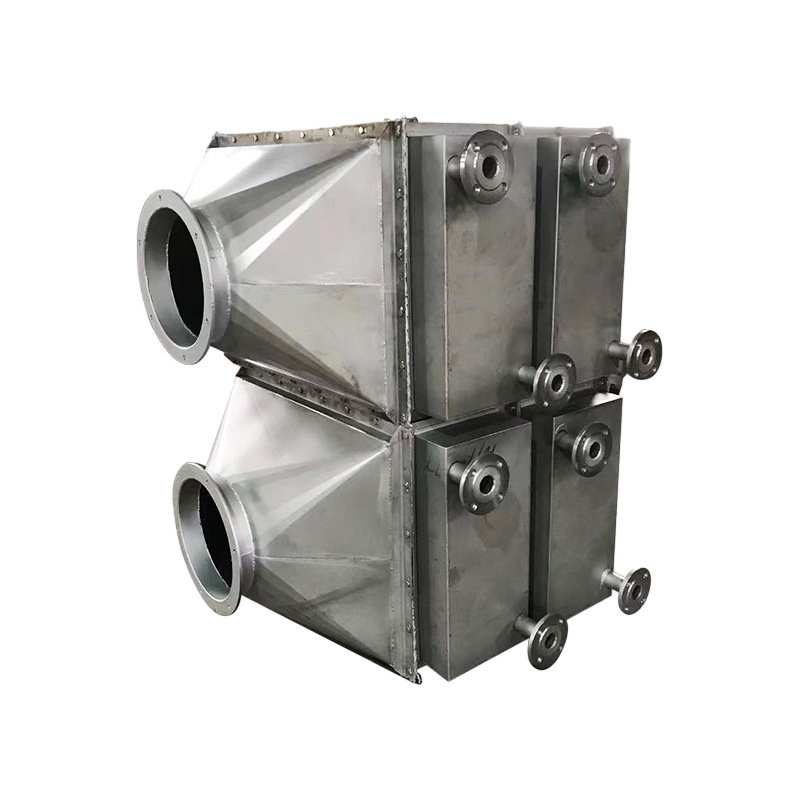
The new type of heat exchanger for boiler economizers uses spiral fin tubes, which not only lowers the boiler flue gas temperature but also fully utilizes the boiler exhaust heat, potentially increasing the boiler thermal efficiency by about 10-15%, significantly saving fuel consumption and reducing operating costs. The equipment is made of corrosion-resistant stainless steel, has an attractive appearance, and a long service life. It is also equipped with flue pipe reducing joints, which can directly connect to the boiler flue outlet, offering flexible installation options, a small footprint, and can be installed either vertically or horizontally.
Application of Boiler Economizers:
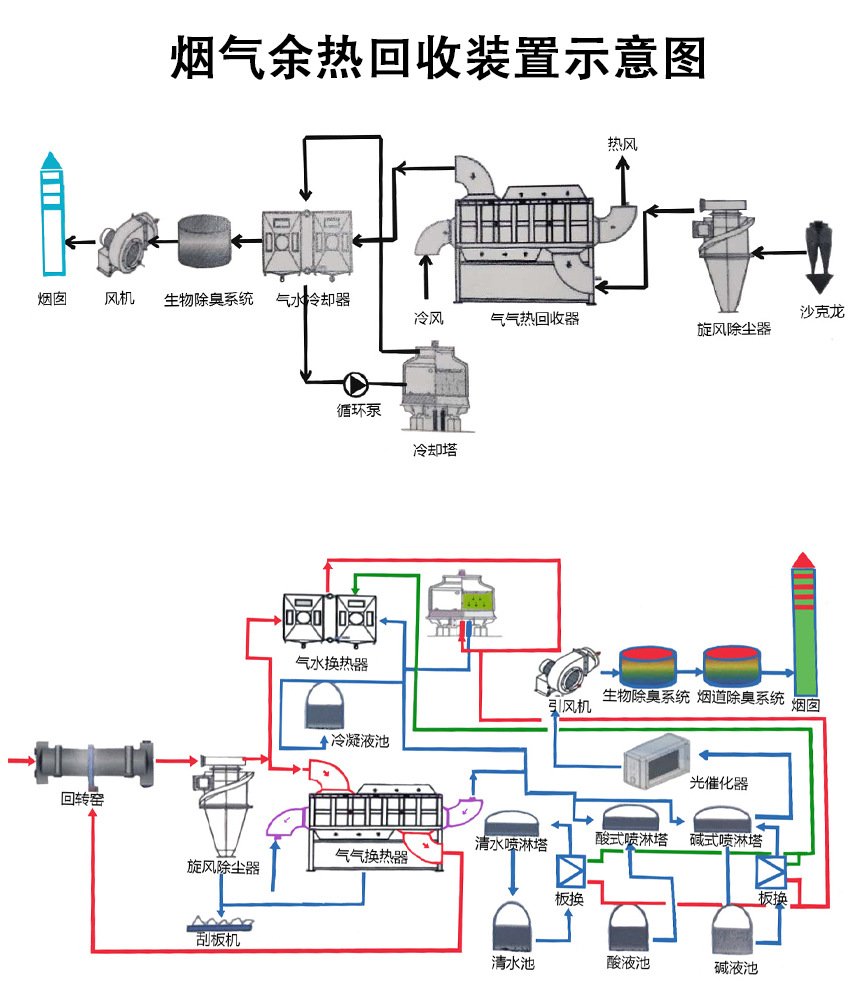
The efficiency of industrial oil-fired, gas-fired, and coal-fired boilers is around 70%. Among the wasted heat, flue gas heat accounts for the majority. Typically, the exhaust temperature at the end of steam and hot water boilers is above 200°C, while the exhaust temperature of heat-conducting oil boilers is between 280°C-350°C. By using waste heat recovery equipment, such as a waste heat boiler, this portion of heat can be recovered and used to increase the boiler feed water temperature, blower temperature, or indirectly heat tap water for domestic use, which can reduce energy consumption and achieve energy savings.
| No. | Feature | Description |
|---|---|---|
| 01 | High-Quality Material Selection | Fine material selection and production; product quality assurance; long service life. |
| 02 | Fine Processing | Mature technology; high-standard production; precision manufacturing. |


Reviews
There are no reviews yet.